Tooling and trial
The mould is cut, fitted and trialled in our own shop. T1 parts are measured against the drawing before production is scheduled.
BAOYUANFENG / PRODUCTION
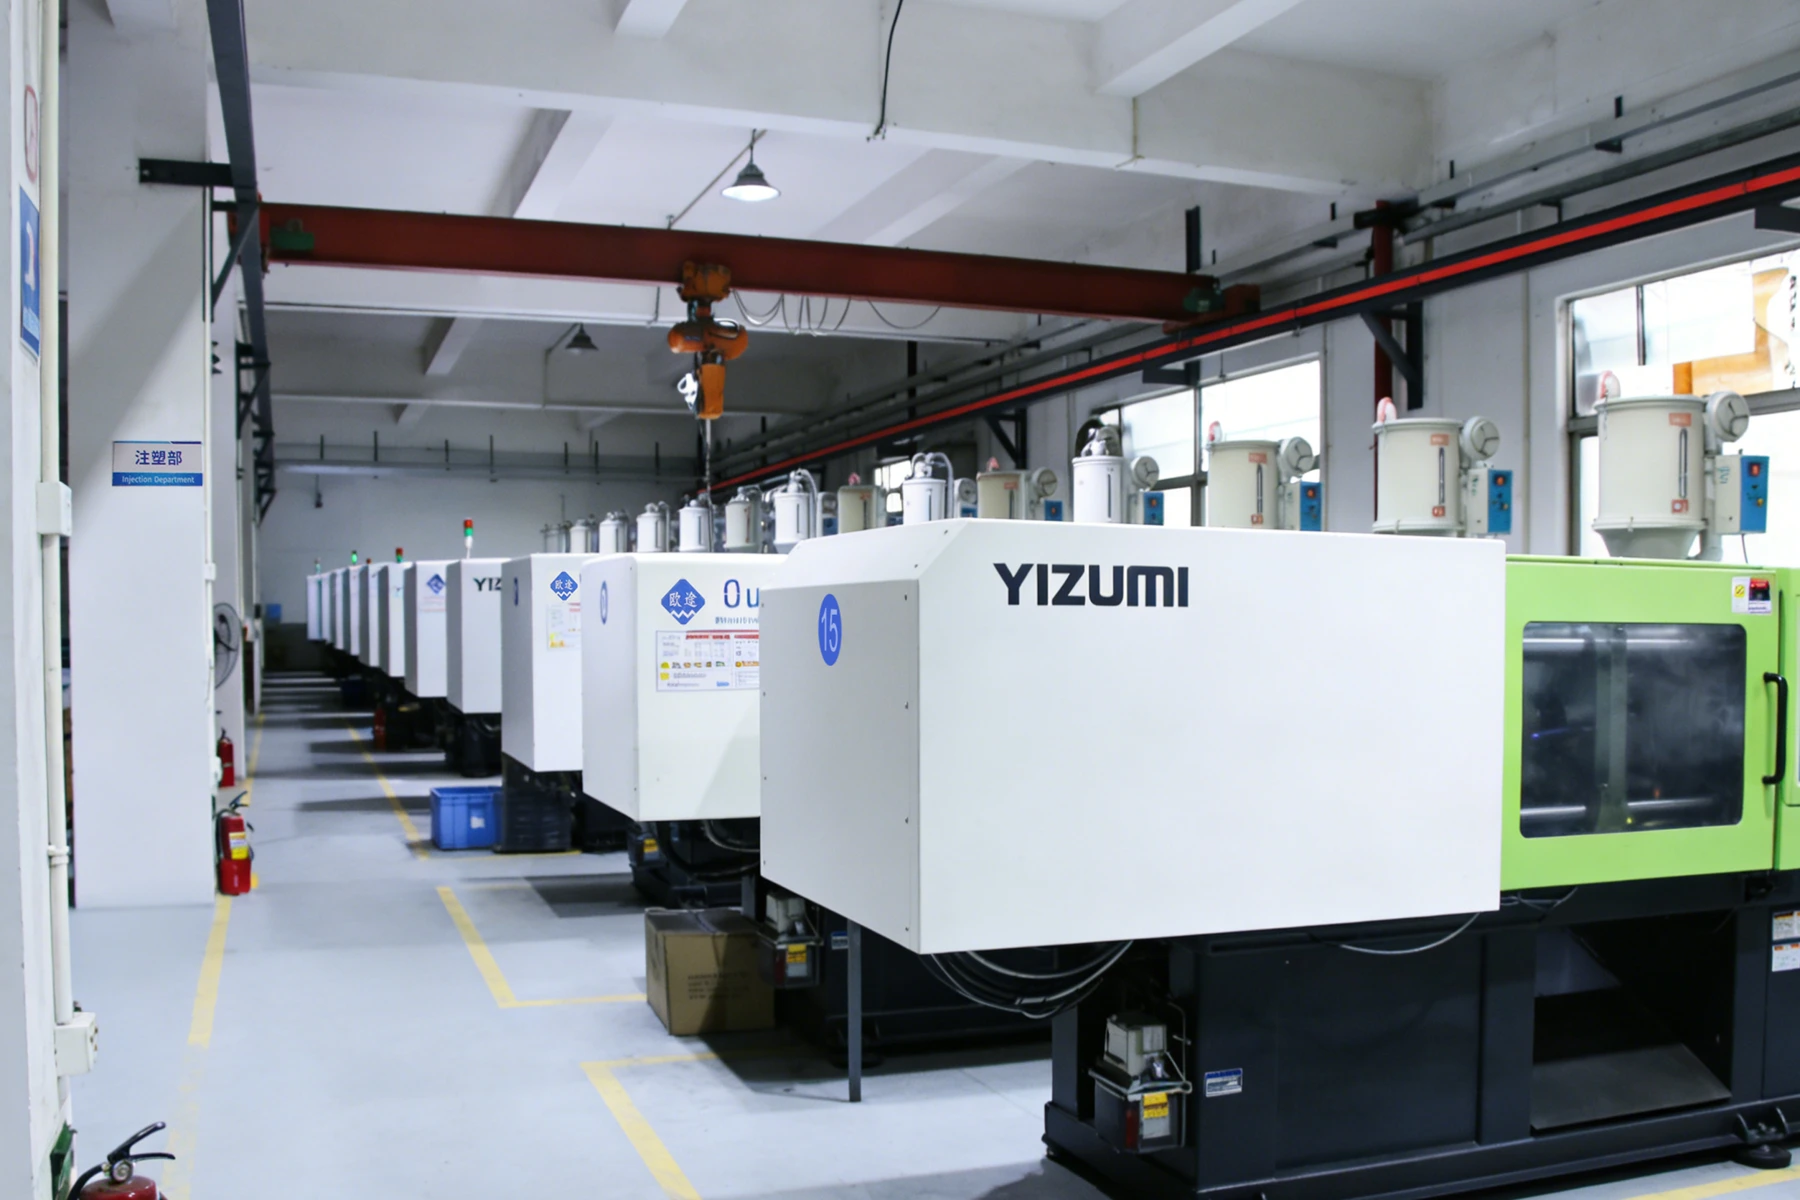
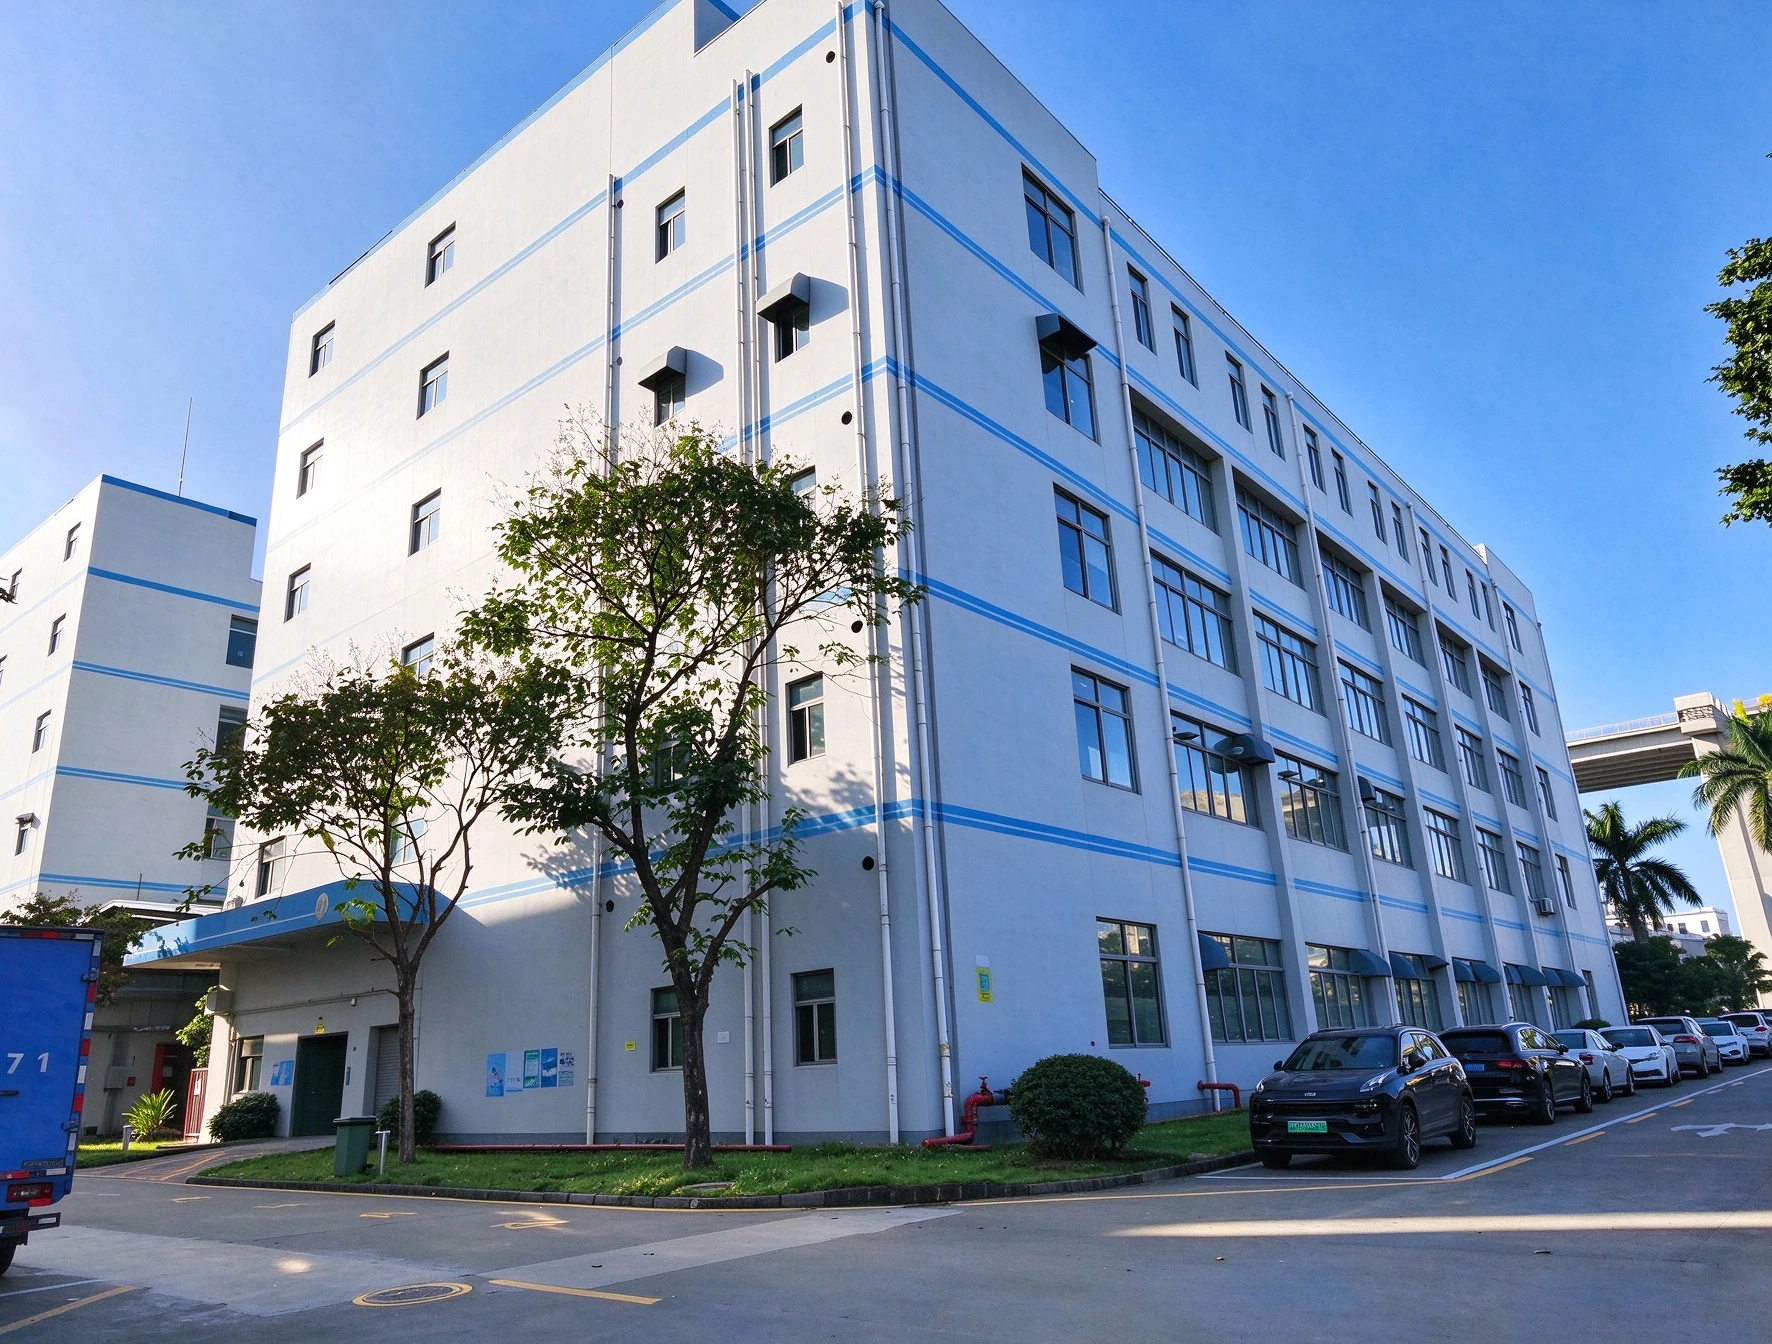
Moulding, decoration, assembly and packing all happen with 3,416 m² of floor space listed on our Alibaba company profile. The production and supply scope is confirmed for each model. This is the eight-step route a cup takes from resin to a sealed carton.
THE ROUTE
The order of these steps is not decorative. A part that will be laser-engraved is moulded to a different surface than one that will be screen printed, and packing is planned before moulding starts, not after.
The mould is cut, fitted and trialled in our own shop. T1 parts are measured against the drawing before production is scheduled.
Resin is checked against the approved grade — PP, AS, PC, Tritan or silicone — and colour is matched to the approved chip under the same light as the sample.
injection moulding equipment, from a 12 oz tumbler to a 5 L ice bucket. Wall thickness, cycle time and gate position are fixed on the setup sheet; first-off parts are kept as the reference.
Lids, sleeves, coasters and ice trays run on silicone compression equipment at an order-specific production plan, trimmed and deflashed by hand where the part needs it.
Gates removed, flash cleaned, then multi-part items assembled — lid to body, seal fitted, straw and plug checked for engagement.
Screen print, UV print, heat transfer, hydro dip, laser or decal. Artwork, colour and position are confirmed against the signed-off proof before the press runs.
AQL sampling by batch size, with the checks the order specifies: dimensions, appearance, lid fit, leak test on assembled units, carton drop and shipping marks.
Inner pack count, carton size and marks, packing list, then the goods move on the shipping method agreed at quotation.
LEAD TIME
A quoted lead time is a production window, not a promise about the whole project. This is the sequence behind it, so you can see which step your own delay would move.
| Stage | Typical duration | What starts the clock |
|---|---|---|
| Sample — existing model | 1–2 days | Model chosen and stock confirmed |
| Sample — decorated | 5–7 days | Artwork approved for print |
| Tooling, if needed | 25–35 days | Drawing approved and deposit received |
| First sample off new tooling | 30–40 days | Drawing approved |
| Mass production | 25–30 days | Deposit cleared <strong>and</strong> artwork approved |
| Production with new tooling | 30–40 days | Trial parts approved |
| Sea freight, Shenzhen to US West Coast | 14–20 days port to port | Vessel departure |
| Express door to door | 7–10 days | Goods ready |
Sometimes, and only if the model already runs and the press has a free slot. A rush run is a scheduling decision made at quotation, with the cost of overtime stated. It is not something that can be promised after an order is placed.
One run per order unless the quantity needs several days of press time. On a long programme we can hold stock and ship against releases, which is agreed as part of the order.
An unresolved artwork question, a colour that does not match the approved chip, or a specification change. In each case the line waits for a written answer instead of guessing — that pause is visible in the delivery date.
CAPACITY, HONESTLY
A factory page that claims unlimited capacity is not useful to a buyer planning a season. This is the shape of our floor.
injection moulding equipment covering tumblers, stemmed glasses, steins, pitchers and ice buckets. Multiple SKUs of the same model can run in parallel if the moulds exist.
silicone compression equipment, an order-specific production plan, for lids, sleeves, coasters and ice trays. Silicone runs are slower per piece than injection and are planned accordingly.
Stainless shakers, openers and similar barware are sourced to the arrangement confirmed per model, and quoted as a separate line with the source stated. We do not claim a metal workshop we do not have.
We only work in plastic and silicone. Anything that needs glass, ceramic, leather or a metal body is either declined or sourced openly — it is not quietly passed off as our own production.
CONTINUE YOUR PROJECT
YOUR NEXT STEP
Model or idea, quantity, decoration, destination and the date the goods must arrive.